
Fixed Ball Valve Applications in Refinery Projects
Fixed ball valve applications in refinery projects are critical to safe, efficient, and reliable flow control in one of the most demanding industrial environments. Refineries handle high pressures, elevated temperatures, corrosive media, abrasive slurries, volatile hydrocarbons, and frequent process cycling. In these conditions, a fixed ball valve is often selected for its strong sealing performance, stable operation, lower operating torque, and suitability for large-diameter, high-pressure service. For plant designers, procurement teams, and maintenance engineers, understanding fixed ball valve applications in refinery projects helps improve system reliability, reduce leakage risk, and support long-term operational performance.
This industry-focused guide explains what a fixed ball valve is, where it is used in refinery projects, what benefits it offers, which specifications matter most, and how it compares with other valve types. The content below is written for direct use in SEO-friendly refinery industry pages, blog posts, directory pages, and product knowledge sections. It is designed to help search engines understand the topic clearly while providing practical information for technical readers.
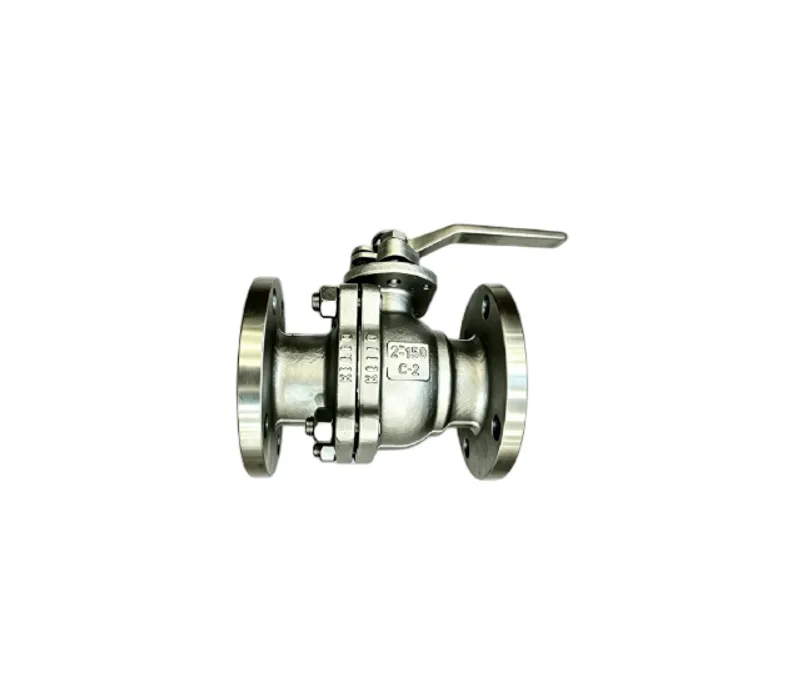
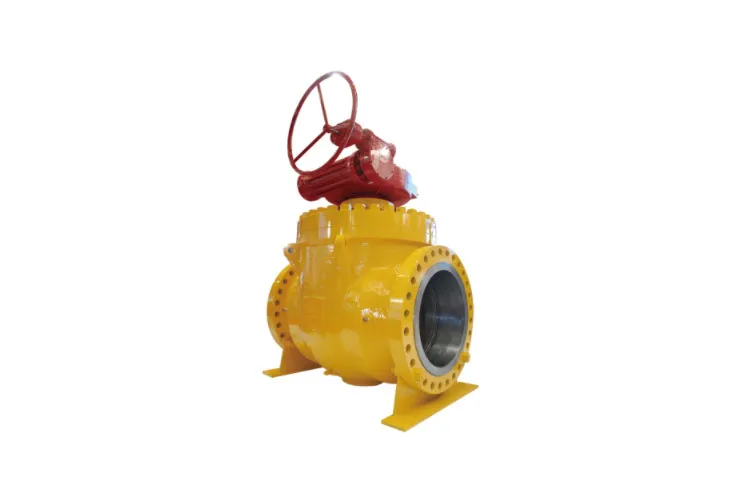
A fixed ball valve, also known as a trunnion-mounted ball valve, is a quarter-turn valve in which the ball is supported by mechanical trunnions or shafts at the top and bottom. Unlike a Floating ball valve, the ball does not rely solely on the seat rings to remain in position. Instead, the fixed structure absorbs pressure load and keeps the ball stable during operation. This design is especially valuable in refinery applications where pressure, pipeline size, and fluid characteristics demand durable and dependable control.
In refinery systems, fixed ball valves are commonly used for on/off isolation, emergency shutoff, line switching, manifold control, and other high-duty service conditions. Their design supports tight shutoff, reduced wear on sealing surfaces, and smoother performance in high-pressure pipelines. Because of these characteristics, fixed ball valves are frequently applied in upstream processing areas, midstream transfer systems, and downstream refinery units.
Refinery projects require valves that can handle demanding process conditions while maintaining consistent sealing and mechanical strength. Fixed ball valve applications in refinery projects are important because these valves help manage crude oil, gas, fuel products, petrochemical feedstocks, water, steam, chemical additives, and process hydrocarbons. In many refinery systems, valve failure can lead to production interruption, safety hazards, environmental issues, and costly shutdowns.
Fixed ball valves are chosen when project engineers need a solution that combines high pressure capability, stable torque behavior, long service life, and secure shutoff. They are especially useful in systems where conventional valves may experience excessive seat loading, leakage, or frequent maintenance needs. Their robust structure makes them suitable for critical service points across refinery infrastructure.
| Advantage | Description | Refinery Benefit |
|---|---|---|
| High Pressure Capability | The ball is mechanically supported, reducing load on the seats. | Suitable for high-pressure pipelines and critical isolation points. |
| Low Operating Torque | Stable ball support helps reduce turning force during operation. | Improves valve actuation efficiency and automation performance. |
| Reliable Shutoff | Seat loading remains consistent for tight sealing. | Helps prevent leakage of hydrocarbons and process fluids. |
| Long Service Life | Reduced wear on sealing components improves durability. | Minimizes downtime and maintenance costs. |
| Bidirectional Sealing | Many fixed ball valve designs can seal in both flow directions. | Useful in complex refinery piping layouts. |
| Large Diameter Suitability | Works well in bigger line sizes where floating valves may be limited. | Common in trunk lines, transfer lines, and main process loops. |
Fixed ball valve applications in refinery projects are found across many process areas. These valves are typically selected for high-pressure isolation and dependable shutoff in systems where flow interruption must be controlled precisely. The following are some of the most common refinery uses.
Crude oil transfer systems often operate under high pressure and variable flow conditions. Fixed ball valves are used to isolate transfer segments, control line routing, and support safe shutdown during maintenance or emergency events. Their strong sealing capability helps reduce fugitive emissions and product loss.
Refinery pipeline stations require valves that can perform reliably under pressure fluctuations. Fixed ball valves are commonly installed at inlet and outlet points to protect process equipment, isolate sections of line, and support pigging operations where applicable.
In processing units handling hydrocarbons, fixed ball valves are used for isolation in piping networks carrying gas, condensate, naphtha, diesel, and other process streams. Their tight shutoff and resistance to pressure loading make them suitable for many unit operations.
Emergency shutdown systems require fast, dependable valve action. Fixed ball valves can be automated for rapid closure to isolate hazardous sections of a refinery in abnormal conditions. This makes them valuable in safety-critical applications.
Storage areas and tank farms need robust isolation valves for loading, unloading, and transfer operations. Fixed ball valves help control the movement of flammable liquids while maintaining a secure seal under frequent operational use.
Some refinery utility systems such as steam, treated water, nitrogen, and instrument gas may also use fixed ball valves depending on pressure and service requirements. Their low torque operation can be beneficial in automated utility networks.
Sour service conditions contain hydrogen sulfide and other aggressive media that require careful material selection. Fixed ball valves used in these applications must meet appropriate material and compliance requirements to ensure safety and corrosion resistance.
Refinery environments are highly variable, and fixed ball valve applications must be matched to the specific service conditions of each process line. Important service factors include pressure class, temperature range, media type, line size, operating frequency, and corrosion exposure. A valve that performs well in one process area may not be suitable for another without proper material and design selection.
| Service Factor | Typical Refinery Requirement | Why It Matters |
|---|---|---|
| Pressure | Low to very high pressure depending on the line | Affects body strength, seat design, and actuator sizing. |
| Temperature | Ambient, elevated, or high-temperature service | Impacts sealing materials and thermal expansion behavior. |
| Media Type | Crude oil, gas, chemicals, steam, water, hydrocarbons | Determines corrosion resistance and sealing compatibility. |
| Corrosion Level | Mild to severe, including sour and corrosive service | Requires suitable metallurgy and surface treatment. |
| Operating Cycle | Occasional or frequent cycling | Influences seat wear and actuator selection. |
| Leakage Class | Often tight shutoff requirements | Important for emission control and process safety. |
Material selection is one of the most important factors in fixed ball valve applications in refinery projects. The valve body, ball, stem, seats, seals, and trim components must all be selected based on process media, temperature, pressure, and corrosion risk. In refinery service, the wrong material choice can lead to premature wear, seat damage, or leakage.
| Component | Common Material Options | Functional Purpose |
|---|---|---|
| Body | Carbon steel, stainless steel, alloy steel | Provides pressure containment and structural strength. |
| Ball | Stainless steel, coated steel, hardened alloy | Ensures smooth rotation and reliable sealing surface. |
| Stem | Stainless steel, alloy steel | Transfers torque from actuator or hand lever to the ball. |
| Seats | PTFE, reinforced PTFE, metal seated designs | Creates the primary sealing interface. |
| Seals | Elastomers, graphite, specialty polymers | Prevents leakage at stem and body joints. |
| Trim | Corrosion-resistant alloys, hardened materials | Supports wear resistance in demanding service. |
Fixed ball valve design features are specifically beneficial in refinery projects because they improve load distribution, sealing consistency, and operational stability. Unlike simpler valve structures, the fixed ball arrangement allows the valve to perform more reliably under severe process conditions. The mechanical support of the ball reduces the risk of seat overload and helps maintain torque stability during service.
When evaluating fixed ball valve applications in refinery projects, engineers typically review a defined set of specifications. These specifications help ensure compatibility with process demands and project standards. The following table provides a general reference for common valve specification categories used in refinery service.
| Specification Category | Typical Options | Selection Consideration |
|---|---|---|
| Valve Type | Trunnion-mounted fixed ball valve | Preferred for high-pressure and large-diameter lines. |
| Size Range | Small to very large diameters | Depends on line size and service application. |
| Pressure Class | ASME Class 150, 300, 600, 900, 1500, 2500 | Must match design pressure of the pipeline. |
| End Connection | Flanged, welded, butt weld, threaded | Chosen based on piping design and maintenance needs. |
| Operation | Manual, gear-operated, pneumatic, electric, hydraulic | Determines automation and control capability. |
| Seat Type | Soft seat, metal seat, fire-safe seat | Selected according to temperature and sealing demand. |
| Leakage Standard | Low leakage or tight shutoff levels | Important for emissions and process integrity. |
| Design Standard | API, ASME, ISO, or project-specific standards | Ensures compliance with refinery engineering codes. |
Both fixed ball valves and floating ball valves are used in industrial flow control, but refinery projects often favor fixed ball valves for larger, higher-pressure, and more demanding applications. The main difference lies in how the ball is supported and how the sealing load is managed. In a floating design, the ball shifts slightly under pressure to press against the downstream seat. In a fixed design, trunnion support stabilizes the ball and transfers load more efficiently.
| Feature | Fixed Ball Valve | Floating Ball Valve |
|---|---|---|
| Ball Support | Supported by trunnions | Ball floats between seats |
| Pressure Suitability | Excellent for high-pressure service | Better suited to lower and moderate pressures |
| Torque | Lower and more stable | Can increase significantly with pressure |
| Size Range | Ideal for large diameters | Often used in smaller sizes |
| Seat Wear | Reduced due to stable support | May increase under higher pressure |
| Refinery Use | Common in critical isolation and high-pressure lines | Used in less demanding process areas |
Refineries often prefer fixed ball valves for critical service because they provide dependable shutoff where leakage is not acceptable. In hydrocarbon processing, even small leaks can create significant safety and environmental concerns. Fixed ball valves are also favored for their ability to maintain consistent seat load and low friction during operation, which is especially important when valves are automated or used in emergency response systems.
Another major reason is that fixed ball valves perform well in pipelines with fluctuating pressure. Their mechanical support reduces the force acting on the seats, helping to extend service life. In refinery projects where line shutdown is expensive and access is difficult, long-term reliability becomes a top priority. Fixed ball valves support this objective by delivering stable performance over many operating cycles.
Many fixed ball valve applications in refinery projects involve automated operation. Depending on the process requirement, a valve may be equipped with a pneumatic actuator, electric actuator, hydraulic actuator, or gear operator. Automation is common in refinery systems because it improves response time, enhances safety, and enables integration with control systems.
Actuator selection must account for valve torque, line pressure, environmental conditions, fail-safe requirements, and control philosophy. In refinery projects, automated fixed ball valves are often integrated into distributed control systems and emergency shutdown systems to improve process reliability and operator safety.
To achieve the best results from fixed ball valve applications in refinery projects, engineers should evaluate several performance-related factors during design and specification. These factors affect not only valve operation but also lifecycle cost and maintenance planning.
Refinery projects commonly require valves to comply with recognized industry standards. While exact requirements depend on the project specification, standards help ensure consistent quality, testing, and performance. Common references include design, pressure, fire-safe, and testing standards used in oil and gas and petrochemical service.
| Standard Category | Typical Purpose |
|---|---|
| Design Standard | Defines valve construction and dimensional requirements. |
| Pressure Standard | Establishes allowable pressure ratings by class. |
| Fire-Safe Standard | Verifies valve performance after fire exposure. |
| Testing Standard | Confirms seat leakage, shell strength, and operational integrity. |
| Material Standard | Specifies acceptable metallurgy and traceability. |
| Emission Standard | Addresses fugitive emission control at stem and body seals. |
Choosing the right fixed ball valve for refinery service requires careful evaluation of process data, piping requirements, and operating philosophy. The following tips can help support better specification decisions.
Fixed ball valves can offer strong maintenance advantages in refinery projects when correctly specified and installed. Their stable mechanical design helps reduce excessive wear, and their reliable shutoff can extend the interval between major interventions. Many refineries value valves that can perform consistently over long operating cycles with minimal unplanned service.
Maintenance teams should still inspect valve seats, stem seals, actuator functions, and external corrosion protection on a routine basis. In critical service, preventive maintenance programs and functional testing can help identify issues before they affect plant operations. Proper lubrication, calibration, and periodic inspection are all important to preserving valve performance.
For search visibility, the topic is closely related to terms such as fixed ball valve, trunnion Mounted Ball valve, refinery valve applications, high pressure ball valve, refinery isolation valve, oil refinery process valve, hydrocarbon valve solutions, industrial ball valve for refinery, fire safe ball valve, and automated ball valve systems. Including these phrases naturally within technical content can help search engines better understand the page focus and improve relevance for refinery and oil and gas searches.
Fixed ball valve applications in refinery projects are essential to safe, efficient, and high-performance flow control. Because refineries operate under demanding conditions, the valve selection process must prioritize pressure capability, sealing integrity, corrosion resistance, automation compatibility, and long-term reliability. Fixed ball valves deliver important advantages in critical isolation, high-pressure service, large-diameter pipelines, and emergency shutdown systems.
For refinery pages, technical blogs, and industry directories, fixed ball valve content should focus on practical uses, standard specifications, material selection, and performance benefits. A well-structured, SEO-friendly article on fixed ball valve applications in refinery projects can support both search engine ranking and user engagement by answering common engineering questions while remaining broad, informative, and industry neutral.
“`
شخص رابط: مکس.سونگ (سونگشان)
عنوان: مدیر کل
موبایل: +86 15611322632
تلفن: +86 10 89282693
ایمیل: international@bvmc.com
آدرس: پلاک ۳، جاده لوهای، شهر پانگژوانگ، منطقه داکسینگ، پکن


حق چاپ © Beijing Valve Factory Co., Ltd
نقشه سایتاین وب سایت از کوکی ها استفاده می کند تا اطمینان حاصل شود که بهترین تجربه را در وب سایت ما به دست می آورید.


 Phone